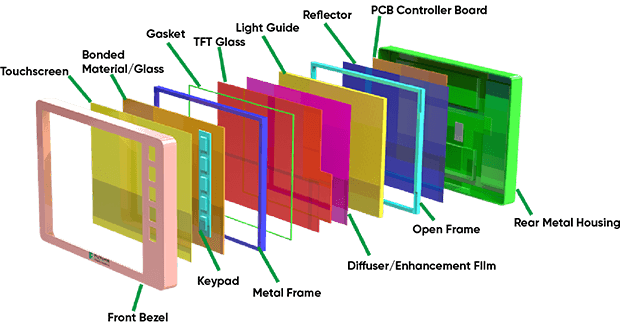
Proprietary backlight engineering that delivers sustained, sunlight-readable brightness up to 2,500 nits — with advanced light management films, custom LED bar design, and thermal management specifically engineered for your enclosure and operating environment. Consistent output across the panel surface. Long lifespan. No hotspots.
Mercury-free, halogen-free high-efficiency LED backlights with 70,000+ hour MTBF, low EMI output, shock and vibration resistance, minimal heat generation, and edge-to-edge brightness uniformity. Fully RoHS compliant. Lower power consumption than CCFL alternatives without any brightness compromise.
Proprietary LCD cell technology, advanced polarizer configurations, and enhancement film stacks that maximize real-world contrast performance — minimizing glare, reducing reflections, and delivering sharp, high-contrast image quality in both direct sunlight and high-ambient indoor environments.
High-efficiency multi-chip LED arrays eliminate power-hungry CCFL inverters, reduce heat generation, and optimize overall system power consumption — extending product lifespan and reducing operating costs without sacrificing brightness or display performance.
Full touch technology integration including projected capacitive (PCAP) multi-touch for intuitive, gesture-based interaction and resistive touch for glove-compatible, wet-environment, and stylus input. Tuned for your specific use case — glove compatibility, waterproof operation, palm rejection, multi-point tracking — with seamless integration into your system’s software environment.
9V to 36V wide-range DC input — adaptable to virtually any system power architecture depending on the engineer's design requirements, whether it's a vehicle platform, outdoor kiosk, industrial machine, or marine installation. A 9V to 36V DC power board is available as an add-on option, with Phoenix connector support for secure, vibration-resistant wiring integration.
AG surface treatment diffuses ambient light to reduce harsh reflections from direct light sources. AR treatment preserves maximum image clarity while increasing light transmission through the display surface. Combined, they deliver clearly readable, high-contrast display performance under any lighting condition — from direct sunlight to indoor fluorescent environments.
Ruggedized display assembly techniques, mechanically reinforced optical bonding, and vibration-tolerant LED backlight design deliver reliable performance in transportation, mining, construction, and harsh industrial environments where standard display assemblies fail under sustained mechanical stress. MIL-STD-810G testing is available upon request through a certified test laboratory for applications requiring formal compliance documentation.
Temperature performance starts at the panel selection stage. Unlike commercial-grade LCD panels rated for 0°C to +50°C, Montek specifies true industrial-grade LCD panels engineered for stable operation across -30°C to +80°C — covering everything from unheated vehicle cabins and cold-storage facilities to high-heat outdoor industrial sites and desert deployments. Consistent contrast, response time, and brightness across the full rated range. No field modifications. No upgrades. The right panel selected from the start.
Completely fanless, passively cooled display configurations that eliminate cooling fan failure, dust infiltration through ventilation, and audible fan noise — while maintaining full display performance in challenging thermal environments through optimized passive heat management.
From IP65 water-resistant front bezels for industrial splash protection through IP68 fully submersion-rated designs for underwater and full immersion applications — Montek provides the right level of waterproof protection for your specific environmental requirements.
Chemically strengthened glass, optically bonded tempered glass, and IK10-rated impact-resistant configurations — providing the physical protection your application demands in public, industrial, or field environments where display damage from impact is a real operational risk.
| LCD panel | Industrial- or commercial-grade, sized and selected for the application |
| Optical bonding | To reduce internal reflections and improve optical performance and durability |
| Air bonding | A cost-conscious integration option where appropriate |
| Touch sensor | PCAP or resistive, selected and tuned for the operating environment |
| Custom cover glass | Shape, thickness, printing, surface treatment, and other project requirements |
| Optional enhancements | AR/AG coatings, EMI shielding, privacy films, IR films, and high-brightness upgrades |
TDM solutions are available for medical, marine, aviation, factory automation, kiosk, vehicle, public transportation, EV charging, digital signage, and other specialized industrial applications.
Optical bonding is a core integration process available for Montek Touch Display Module (TDM) solutions.
We integrate LCD panels, touchscreens, and custom cover glass into complete TDM assemblies for OEM and industrial applications. This process can eliminate the air gap between display layers, helping reduce internal reflections and improve readability, contrast, durability, and overall optical performance.
Depending on the project, brightness enhancement, AR/AG treatments, EMI shielding, optical films, and other display technologies may also be incorporated into the same module.
Tell Montek what your application demands — environment, performance targets, form factor constraints, integration requirements. We’ll engineer a custom display solution that hits every specification and delivers on a schedule that keeps your project moving.